Glass bending and melting demand more than heat; they demand control. A few degrees, seconds, or millimeters can change the final shape. During production, engineers may see edge lift, roller waves, optical distortion, or sudden cracks after cooling. These defects often appear minor beside a large furnace. They are not minor to a customer inspecting a sunlit façade.
So, what causes glass deformation during bending and melting? The answer usually involves uneven temperature distribution, unstable viscosity, gravity, thermal stress, and inconsistent furnace movement. The European Commission’s Best Available Techniques Reference Document for the Manufacture of Glass identifies melting and conditioning as critical stages requiring controlled heat transfer and residence time. Typical soda-lime glass melts near 1,400–1,600°C, although the exact range depends on composition and furnace design. Small temperature differences can therefore create major viscosity differences across one sheet.
Industry standards reinforce this concern. ASTM C1048 addresses heat-treated flat glass and emphasizes quality control for strength, distortion, and surface condition. The National Fenestration Rating Council also evaluates visual quality in completed glazing systems, where roller wave and bow become noticeable under reflected light. These references offer a reliable foundation, but factory results remain imperfect. Batch moisture, burner balance, roller alignment, and cooling airflow can shift from one production run to another.
Practical prevention begins with measurement, not guesswork. Infrared mapping, calibrated thermocouples, viscosity checks, and regular roller inspections can expose hidden process drift. This guide examines how deformation develops and how operators can reduce it through thermal uniformity, mechanical alignment, and disciplined cooling control.
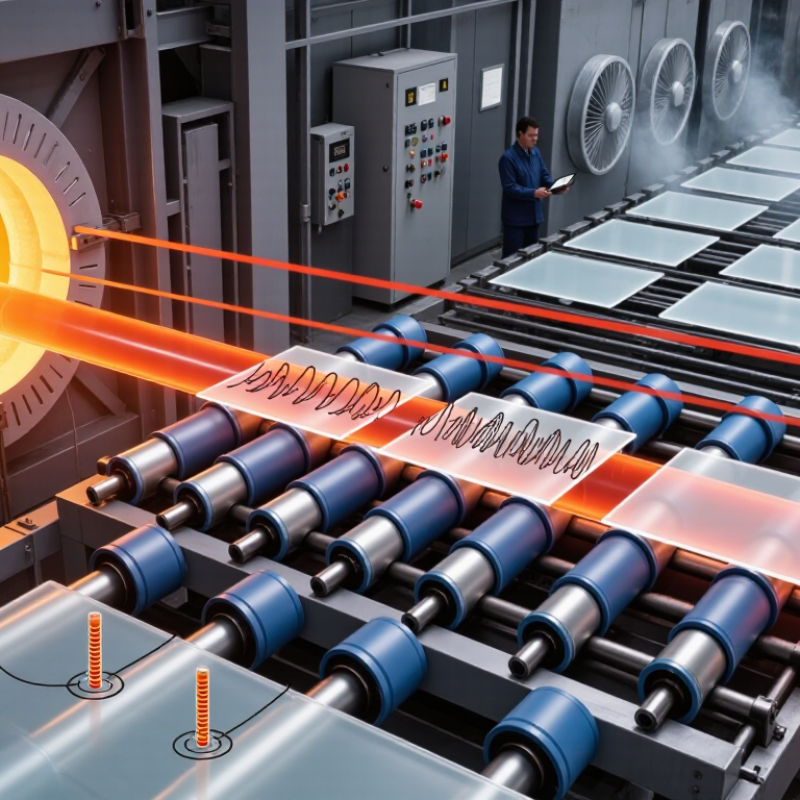
Define Soda-Lime Glass Limits: 10^14.5, 10^13, and 10^6.6 Pa·s
How to Prevent Glass Deformation During Bending and Melting
Soda-lime glass does not have one fixed working temperature. Its viscosity changes continuously as heat rises. Industry references commonly place the strain point near 10^14.5 Pa·s, the annealing point near 10^13 Pa·s, and the softening point near 10^6.6 Pa·s. ASTM C336 and ASTM C338 describe standard methods for measuring these critical properties.
At 10^14.5 Pa·s, internal stress begins to relax very slowly. Cooling too quickly below this range can freeze stress into the glass. Near 10^13 Pa·s, annealing becomes practical because molecular movement is faster. Hold time still depends on thickness, furnace uniformity, and temperature history. A thick panel may need much longer than a thin sheet.
Bending usually occurs close to the 10^6.6 Pa·s softening range, but this value is not a universal forming recipe. Excess heat can cause edge sagging, waviness, or unwanted thinning. In production trials, measure the actual glass temperature, not only the furnace setting. NIST glass-property references also warn that viscosity values vary with composition and measurement method. That matters more than many operators expect.
A useful control plan is simple: approach the forming range gradually, support the glass evenly, and cool through the annealing zone under stable airflow. Recheck the profile after each trial. The first setting is rarely perfect. Small differences in alkali content, sheet thickness, or tooling clearance can shift deformation behavior noticeably.
How to Prevent Glass Deformation During Bending and Melting
Soda-lime glass processing limits are commonly defined by viscosity. As temperature rises, viscosity decreases and the risk of bending, sagging, or uncontrolled deformation increases.
Strain Point
1014.5 Pa·s
Typical reference temperature: about 510°C. Internal stresses are effectively frozen below this range.
Annealing Point
1013 Pa·s
Typical reference temperature: about 548°C. Stress relief occurs efficiently near this viscosity.
Softening Point
106.6 Pa·s
Typical reference temperature: about 720°C. Glass begins to deform readily under its own weight.
To minimize deformation, heat uniformly, control the dwell time near the softening range, support the glass adequately, and cool gradually through the annealing range. Actual temperatures vary with composition, thickness, heating rate, and thermal history.
Bend Glass Around 600–700°C with Continuous Support to Prevent Sagging
Bending glass at 600–700°C demands continuous support, not occasional contact. In this range, soda-lime glass becomes highly viscous and begins flowing under its own weight. ASTM C372 data places its thermal expansion near 9 × 10⁻⁶/K, so uneven heating can create stress and shape distortion. The exact forming temperature still depends on thickness, composition, and furnace design.
Use a clean, level support bed throughout heating, transfer, bending, and cooling. Refractory rollers or shaped ceramic fixtures should contact the glass evenly, with no sharp pressure points. Keep the support surface aligned with the intended radius. A small gap can become a visible wave when the panel softens. Support must never stop.
Temperature mapping is essential. Industry furnace studies commonly recommend controlling hot-zone variation within a few degrees for repeatable forming, although real tolerances depend on the product. Measure both the glass surface and furnace atmosphere. Reduce temperature gradients before increasing forming speed. During cooling, maintain support through the strain and annealing ranges; ASTM C598 testing principles show why uncontrolled cooling can lock in stress. I have seen operators focus on the bend and neglect the exit path. That mistake often causes delayed sagging or edge cracks. Continuous support helps, but it cannot correct poor heating, dirty fixtures, or an inaccurate temperature reading.
How to Prevent Glass Deformation During Bending and Melting - Bend Glass Around 600–700°C with Continuous Support to Prevent Sagging
| Glass Type |
Typical Annealing Point |
Typical Softening Point |
Practical Bending Range |
Support Requirement |
Main Deformation Risk |
| Soda-lime float glass |
Approximately 540–550°C |
Approximately 700–730°C |
600–700°C |
Use a continuous, level refractory bed or closely spaced supports across the entire heated area. |
Sagging, edge curling, uneven curvature, and thickness distortion. |
| Low-iron soda-lime glass |
Approximately 540–550°C |
Approximately 700–730°C |
600–700°C |
Provide uniform support and balanced heating; transparent glass makes local hot spots harder to detect visually. |
Localized softening, optical distortion, and non-uniform bending. |
| Borosilicate glass |
Approximately 560°C |
Approximately 820°C |
Usually above 750°C |
Use a rigid heat-resistant mold or continuous support because the glass requires higher forming temperatures. |
Insufficient forming, thermal gradients, and cracking during uneven cooling. |
| Fused silica |
Approximately 1,050°C |
Approximately 1,580°C |
Typically above 1,100°C |
Use high-temperature tooling designed for silica processing; ordinary glass-bending supports are unsuitable. |
Inadequate deformation, thermal shock, and contamination from unsuitable tooling. |
Recommended Process Controls for Soda-Lime Glass
| Control Parameter |
Suggested Starting Range |
Purpose |
Deformation-Prevention Practice |
| Bending temperature |
600–700°C |
Softens soda-lime glass sufficiently for controlled forming. |
Use the lowest temperature that achieves the required curvature; avoid prolonged exposure near the upper end of the range. |
| Support spacing |
Continuous support preferred; otherwise use closely spaced supports |
Reduces unsupported span and bending under the glass's own weight. |
Keep the support surface level, clean, and aligned with the intended bending profile. |
| Temperature uniformity |
Minimize hot and cold zones |
Prevents one region from becoming softer than another. |
Use multiple temperature measurements across the glass and allow adequate heat-soak time. |
| Heating rate |
Controlled and material-dependent |
Limits thermal gradients and reduces stress before forming. |
Use slower heating for thicker sheets, complex shapes, and assemblies with different materials. |
| Cooling and annealing |
Cool gradually through the strain range |
Relieves internal stress and helps preserve the formed shape. |
Do not remove support while the glass is still hot enough to deform; follow a controlled annealing cycle. |
| Tooling contact |
Clean, compatible, and heat-resistant |
Prevents sticking, surface damage, and contamination. |
Use suitable refractory materials and verify that the mold does not restrict uniform thermal expansion. |
Note: Temperature values are typical working ranges and vary with glass composition, thickness, heating equipment, curvature, and tooling. Confirm the correct cycle using the glass supplier's technical data and a small test piece before production.
Conclusion
What causes glass deformation during bending and melting? The main factors are insufficient viscosity control, uneven heating, thermal expansion, and cooling too quickly. For soda-lime glass, deformation should be managed by recognizing key viscosity limits: approximately 10^14.5 Pa·s near the strain range, 10^13 Pa·s during annealing, and about 10^6.6 Pa·s when the glass becomes suitable for forming. Melting should remain close to 1450–1550°C to promote a uniform, homogeneous material rather than localized soft spots.
During bending, heat the glass gradually to around 600–700°C and provide continuous support so gravity does not cause sagging or distortion. Because soda-lime glass expands at roughly 9×10^-6/K, controlled temperature changes are essential for reducing internal stress. After shaping, anneal the glass at approximately 540–550°C, then cool it slowly and evenly through temperatures below the 510°C strain point. This staged process helps preserve the intended shape, improve strength, and reduce the risk of cracking or permanent deformation.
 Yabo CNC
